Multi-Hardness EVA & Thick Material Cutting Test (ZCRA1410/ZCRC1410)
Trusted by 6,000+ customers worldwide
Multi-Hardness EVA & Thick Material Cutting Test (ZCRA1410/ZCRC1410)
Test Overview
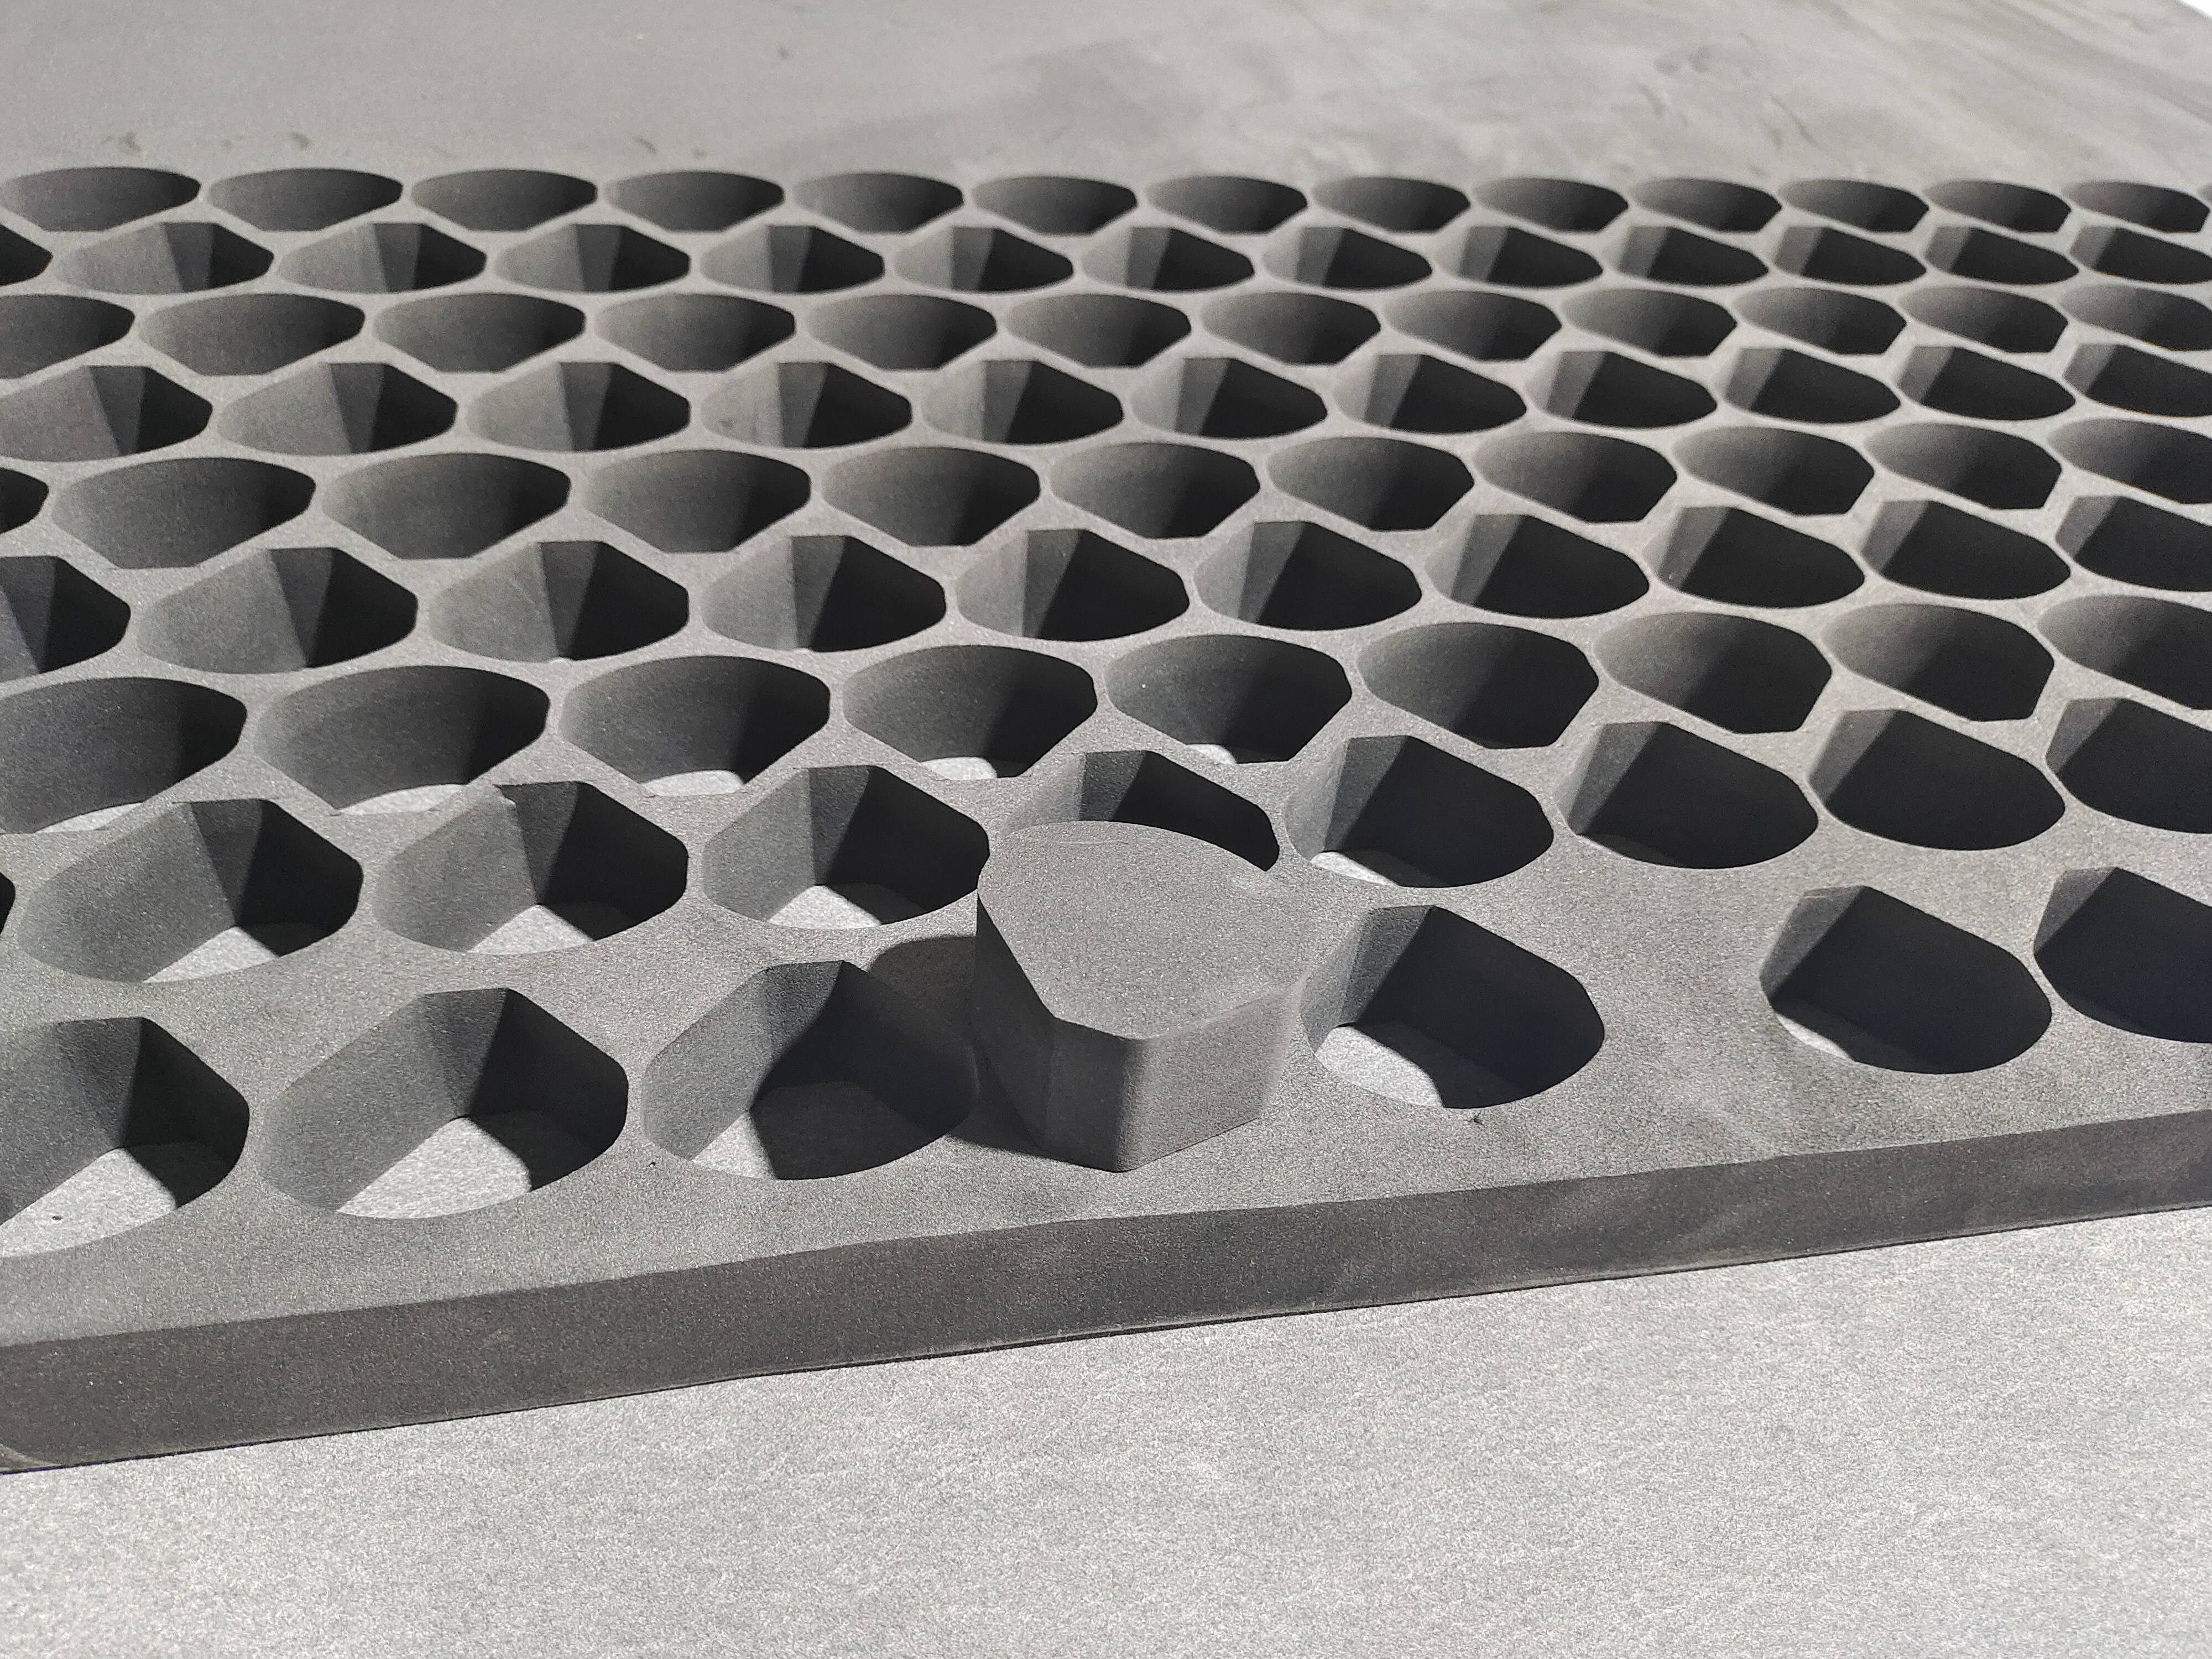
Material: 38°/45°/70° EVA foam
Equipment: ZCCUTTER ZCRA1410 / ZCRC1410
Tool: 10mm high-amplitude pneumatic oscillating knife
Result: Regular hardness (38°/45°/70°) cutting successful with clean edges and normal waste removal; 100mm thick material prototyping encountered challenges (blade breakage, difficult waste removal).
Equipment Configuration & Core Technology
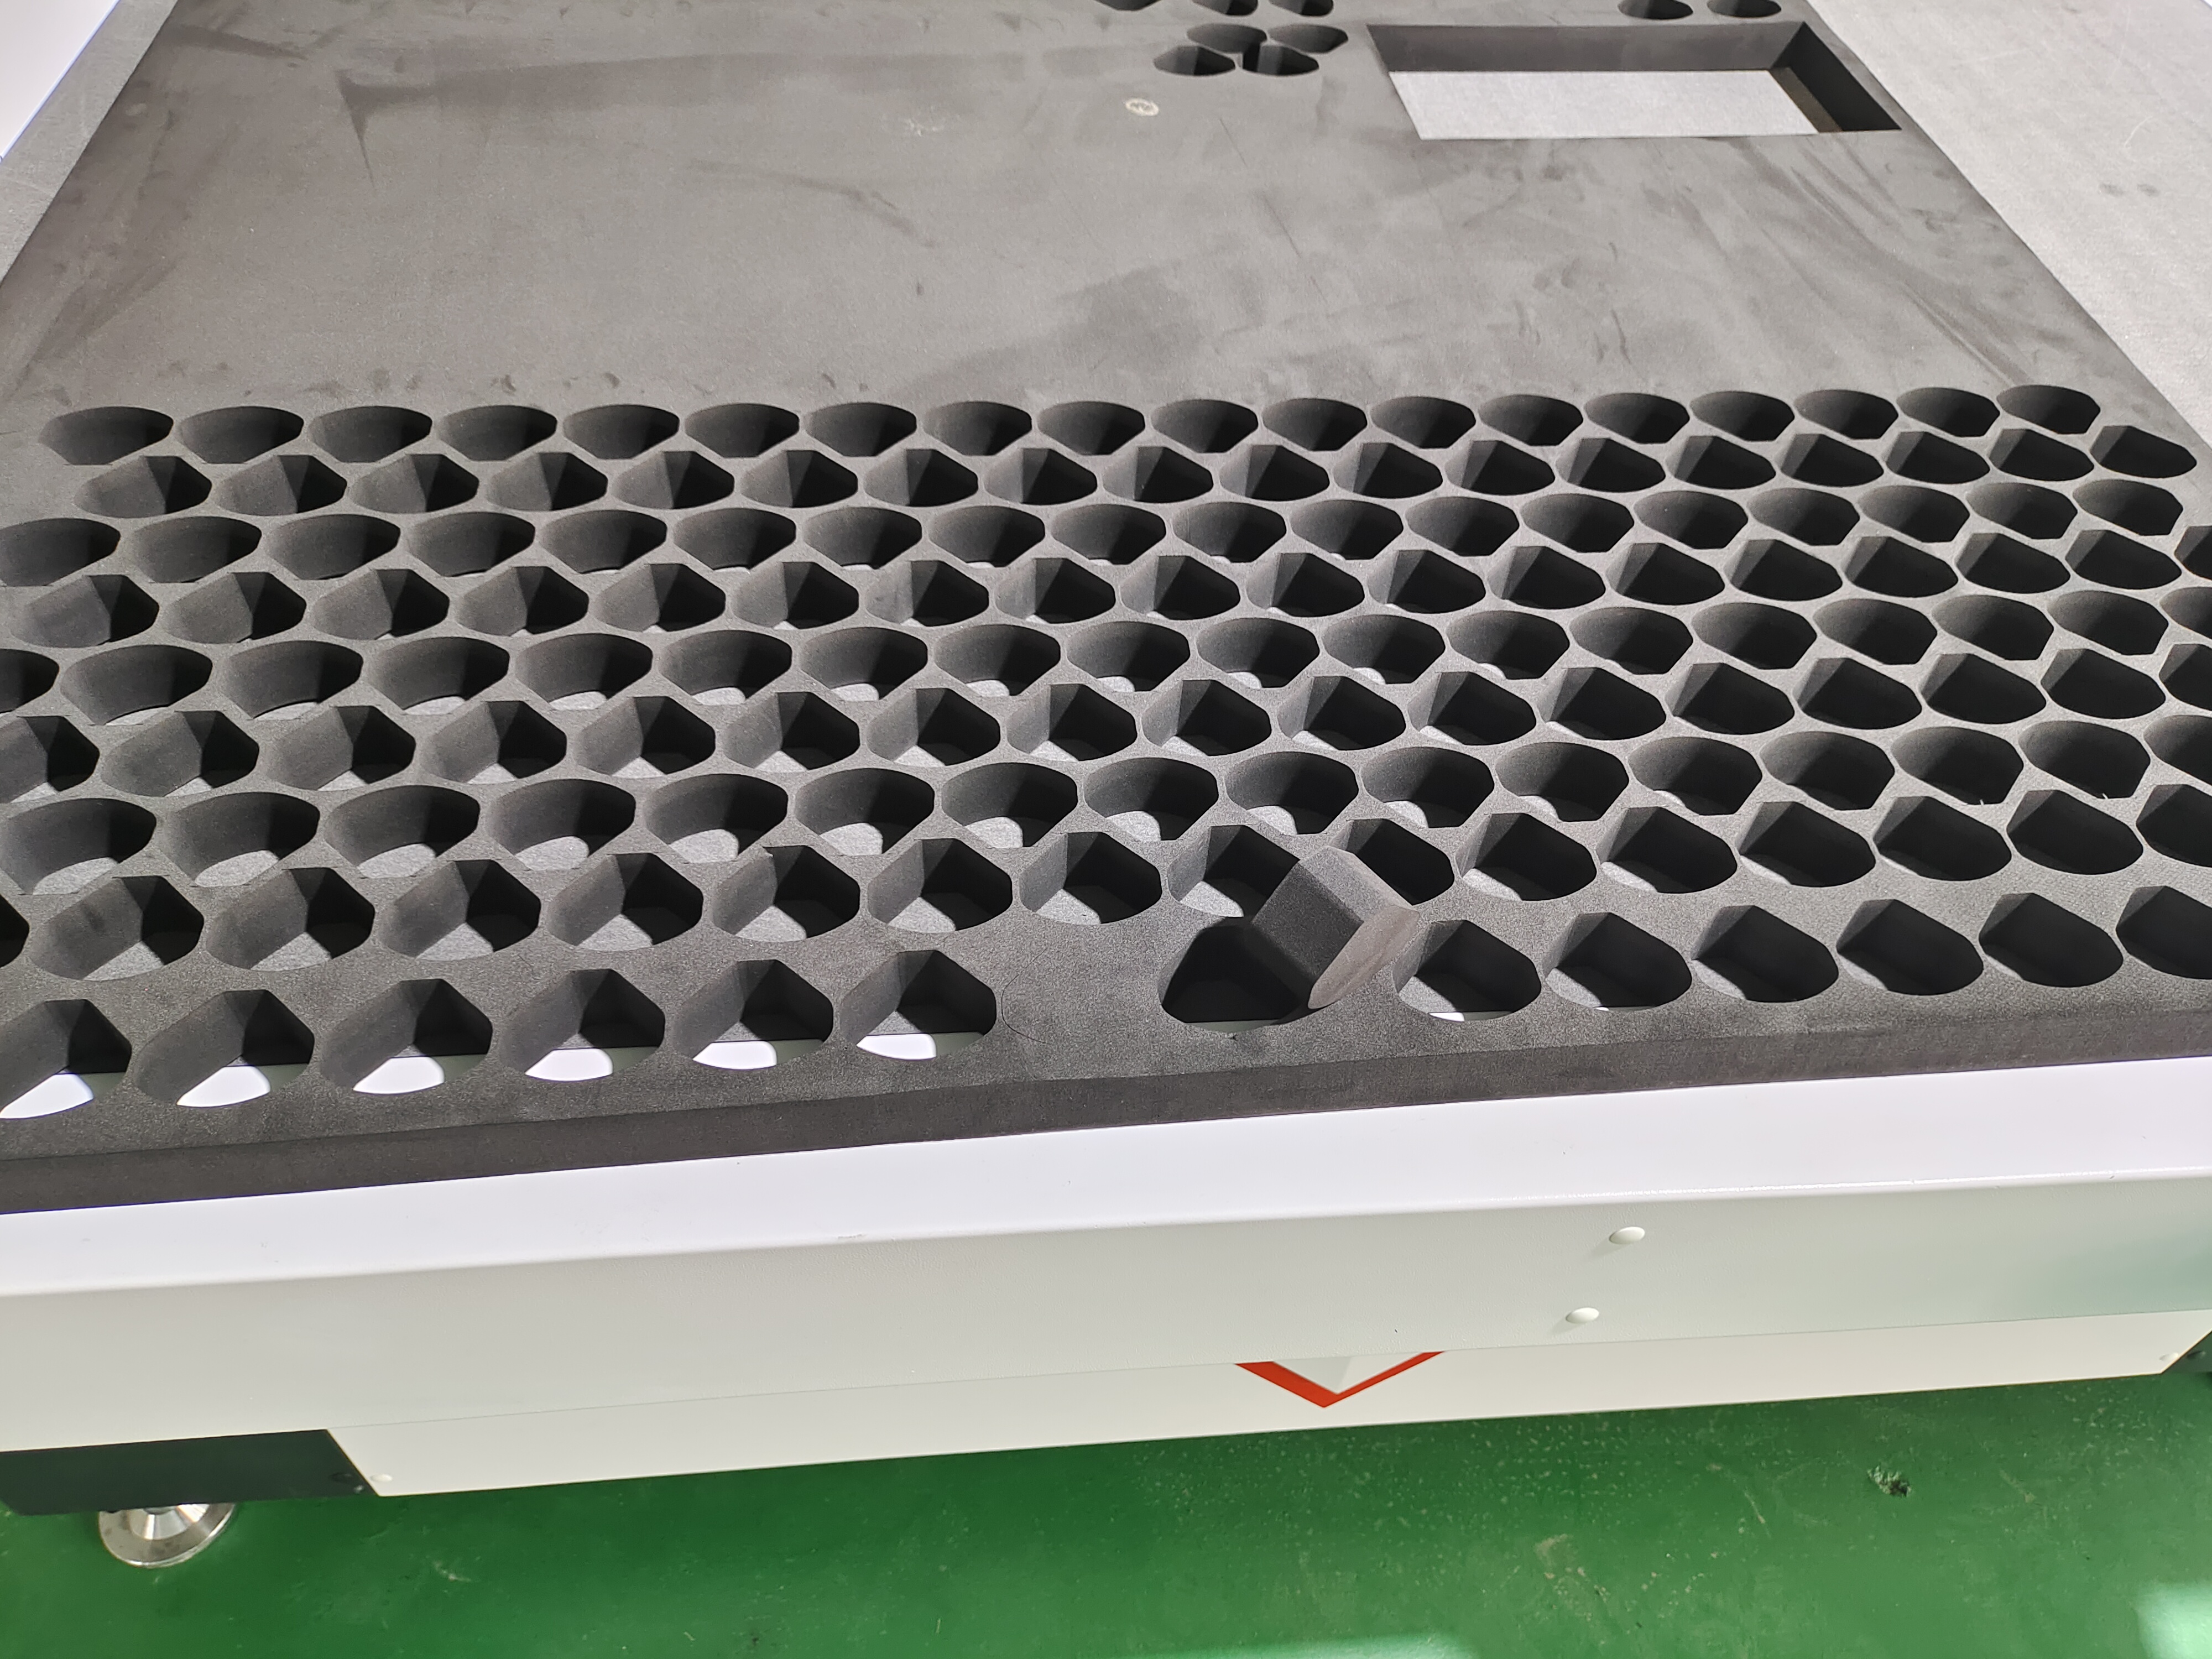
ZCCUTTER flexible CNC cutting machine comes standard with Delta servo motors, HIWIN linear guides, and Zhongrui closed-loop CNC system, combined with dual closed-loop Z-axis depth control and 20MP four-point CCD vision positioning. This test used ZCRC1410 to complete cutting samples for 38° (precision drilling/cutting), 45° and 70° EVA foam, with finished products showing clean edges and normal waste removal.
38° EVA Precision Cutting (Drilling/Complex Shapes)
38° EVA is a soft foam material. ZCRC1410 completed precision hexagonal hole array cutting, with uniform hole spacing and clean edges without burrs or collapse. Precision drilling of soft materials requires extremely high tool amplitude and downward speed control. This test verified the equipment's fine processing capability on low-hardness materials.
45° EVA Strip Cutting
45° EVA is a medium-hardness foam material. ZCRC1410 completed strip cutting, with uniform strip width and good edge perpendicularity. Cutting medium-hardness materials requires high tool penetration force and travel stability. This test verified the equipment's batch processing capability on medium-hardness materials.
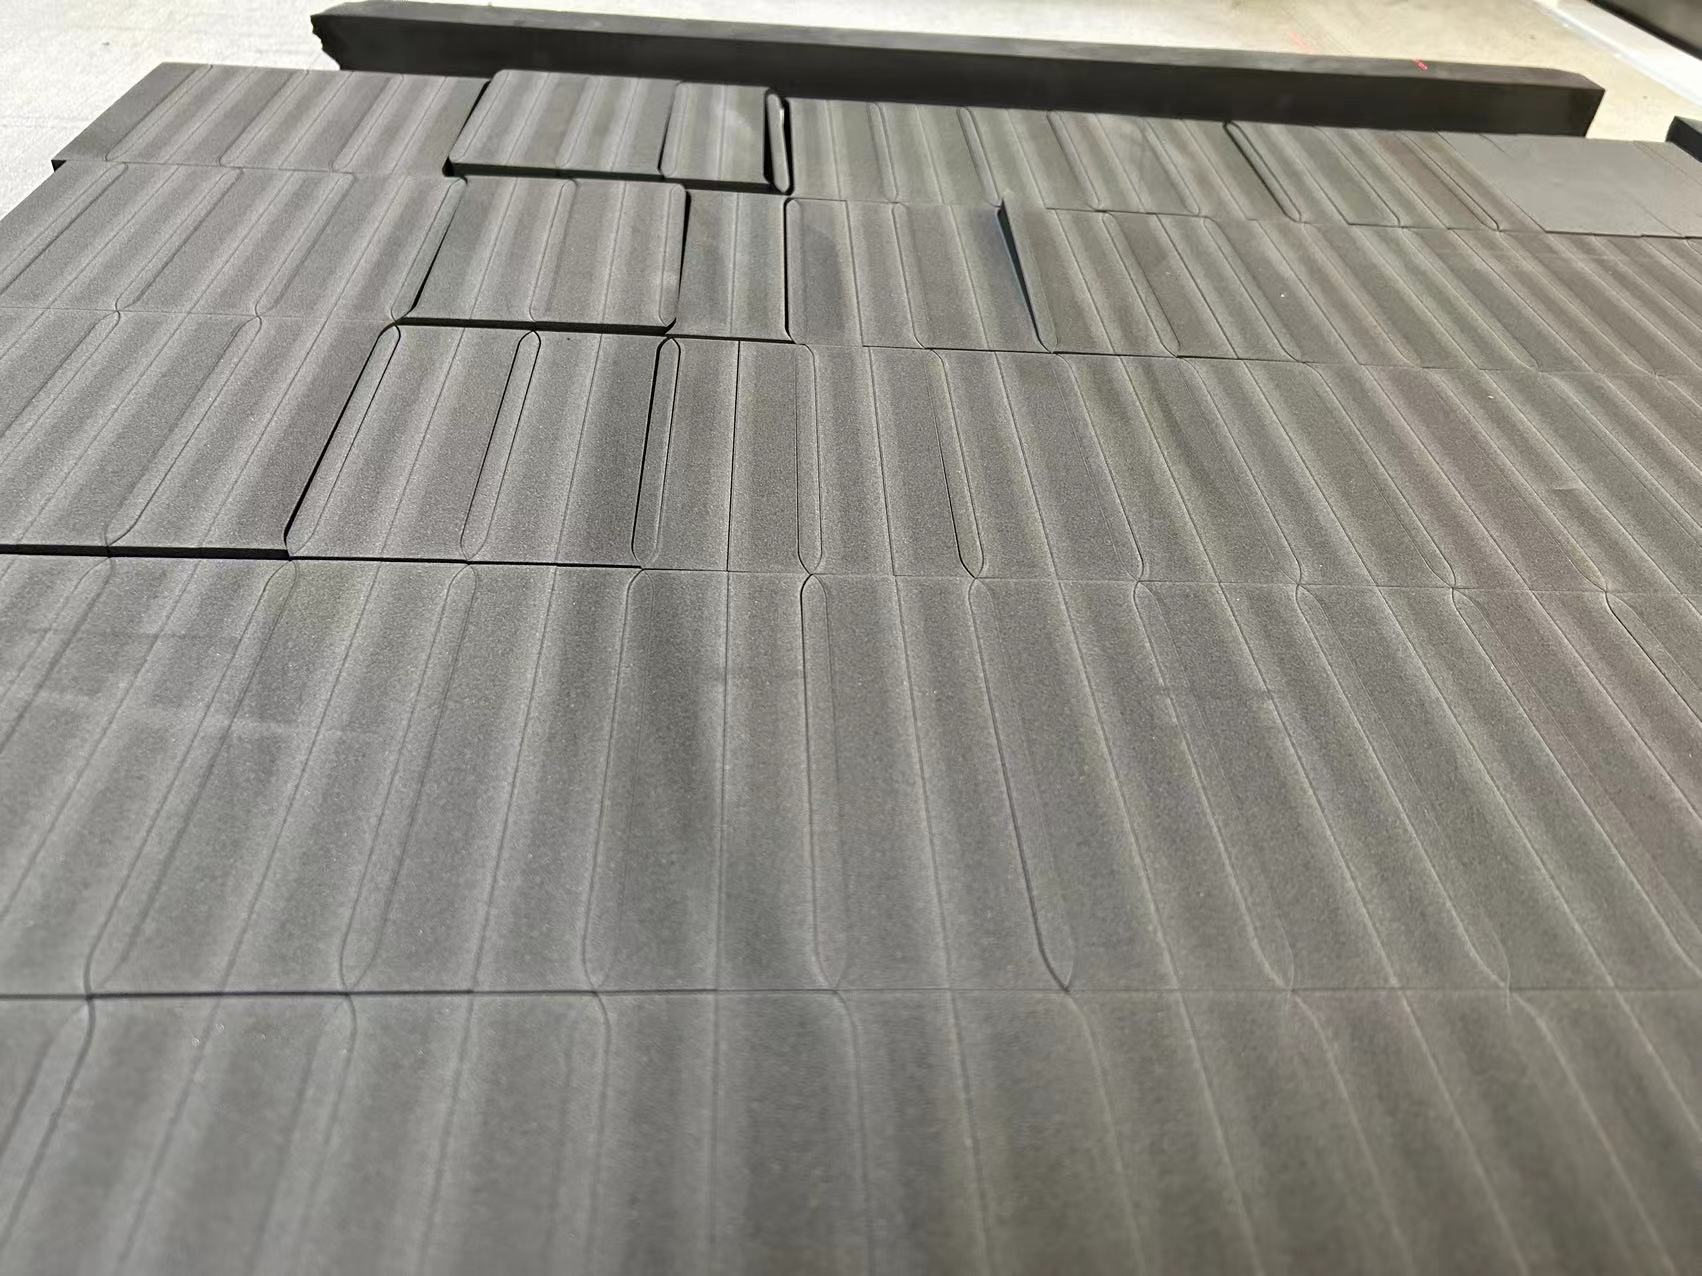
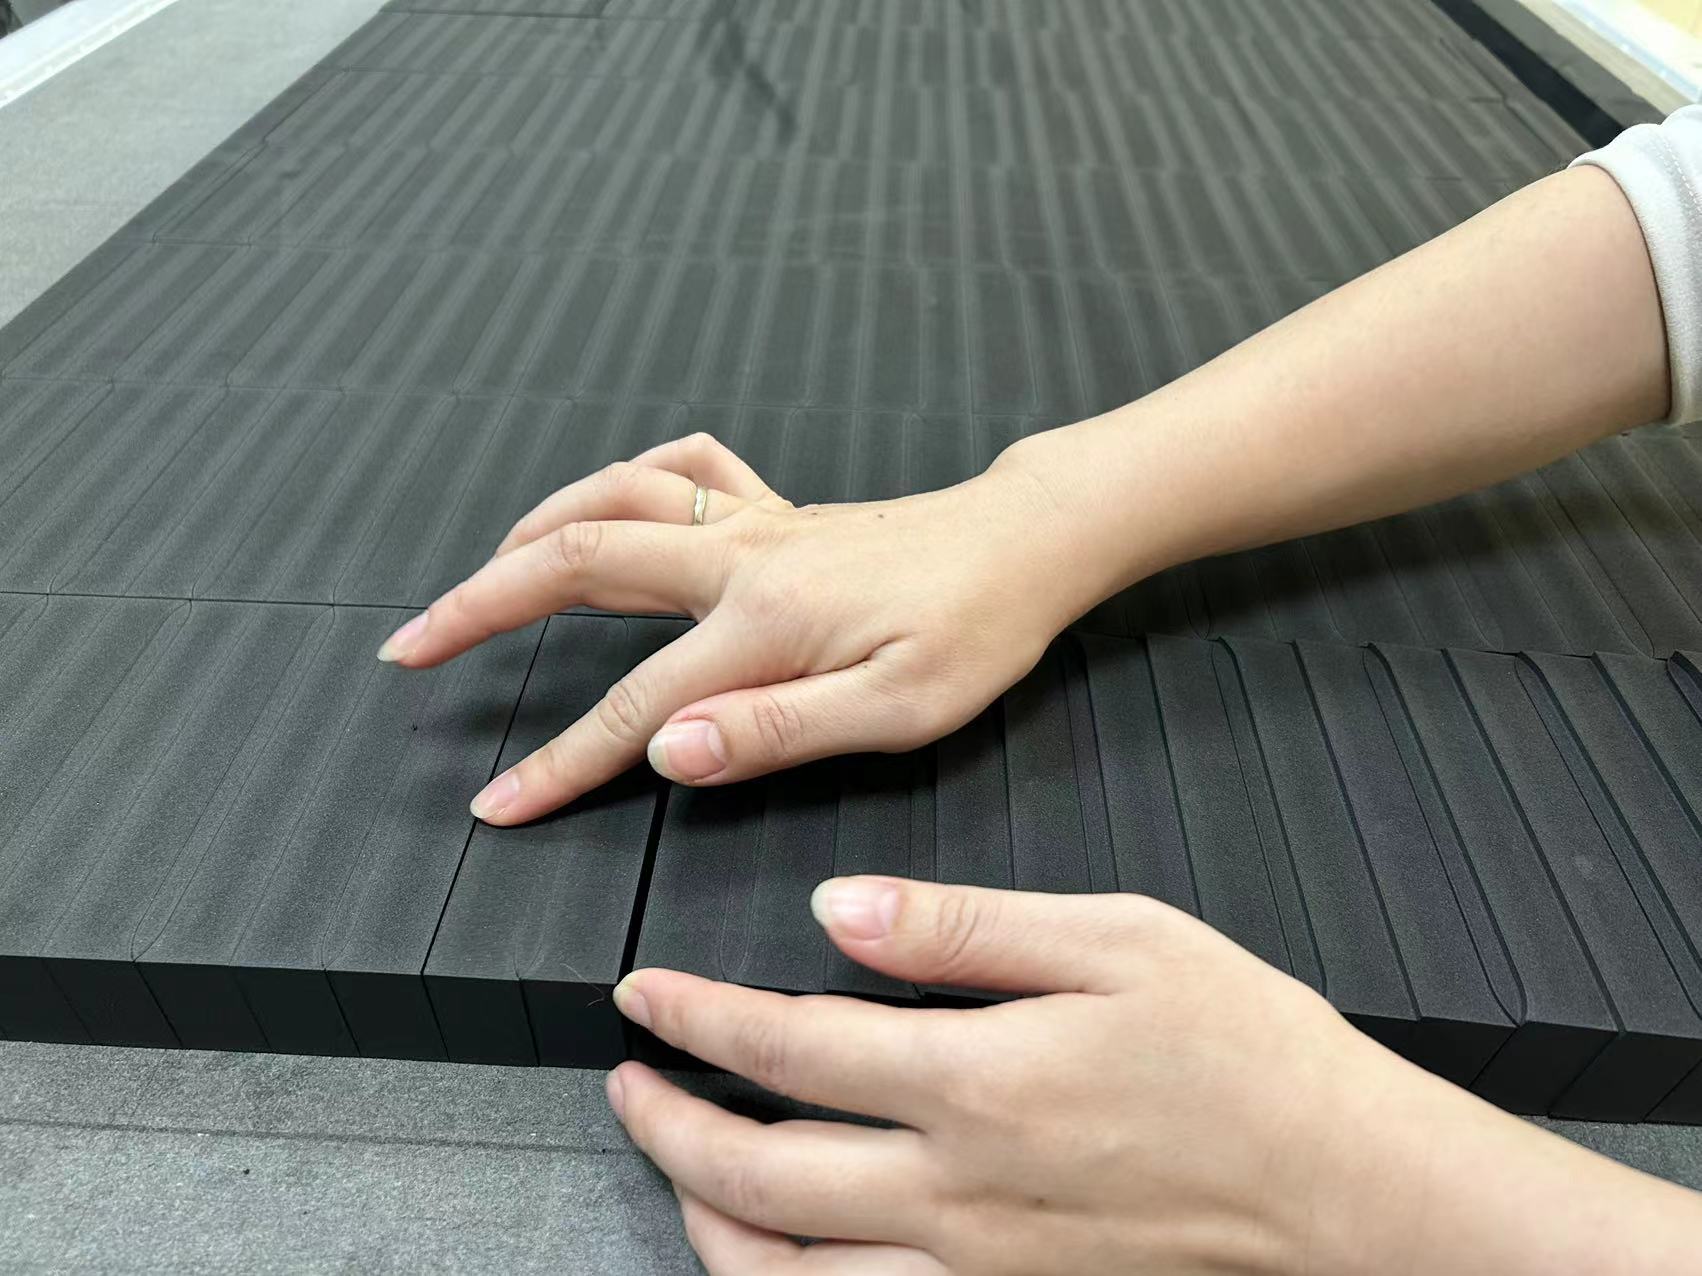
70° EVA Rectangular Block Cutting
70° EVA is a high-hardness foam material. ZCRC1410 completed rectangular block cutting, with precise block dimensions and sharp corners. High-hardness materials require higher tool wear resistance and cutting pressure. This test verified the equipment's forming capability on high-hardness materials.
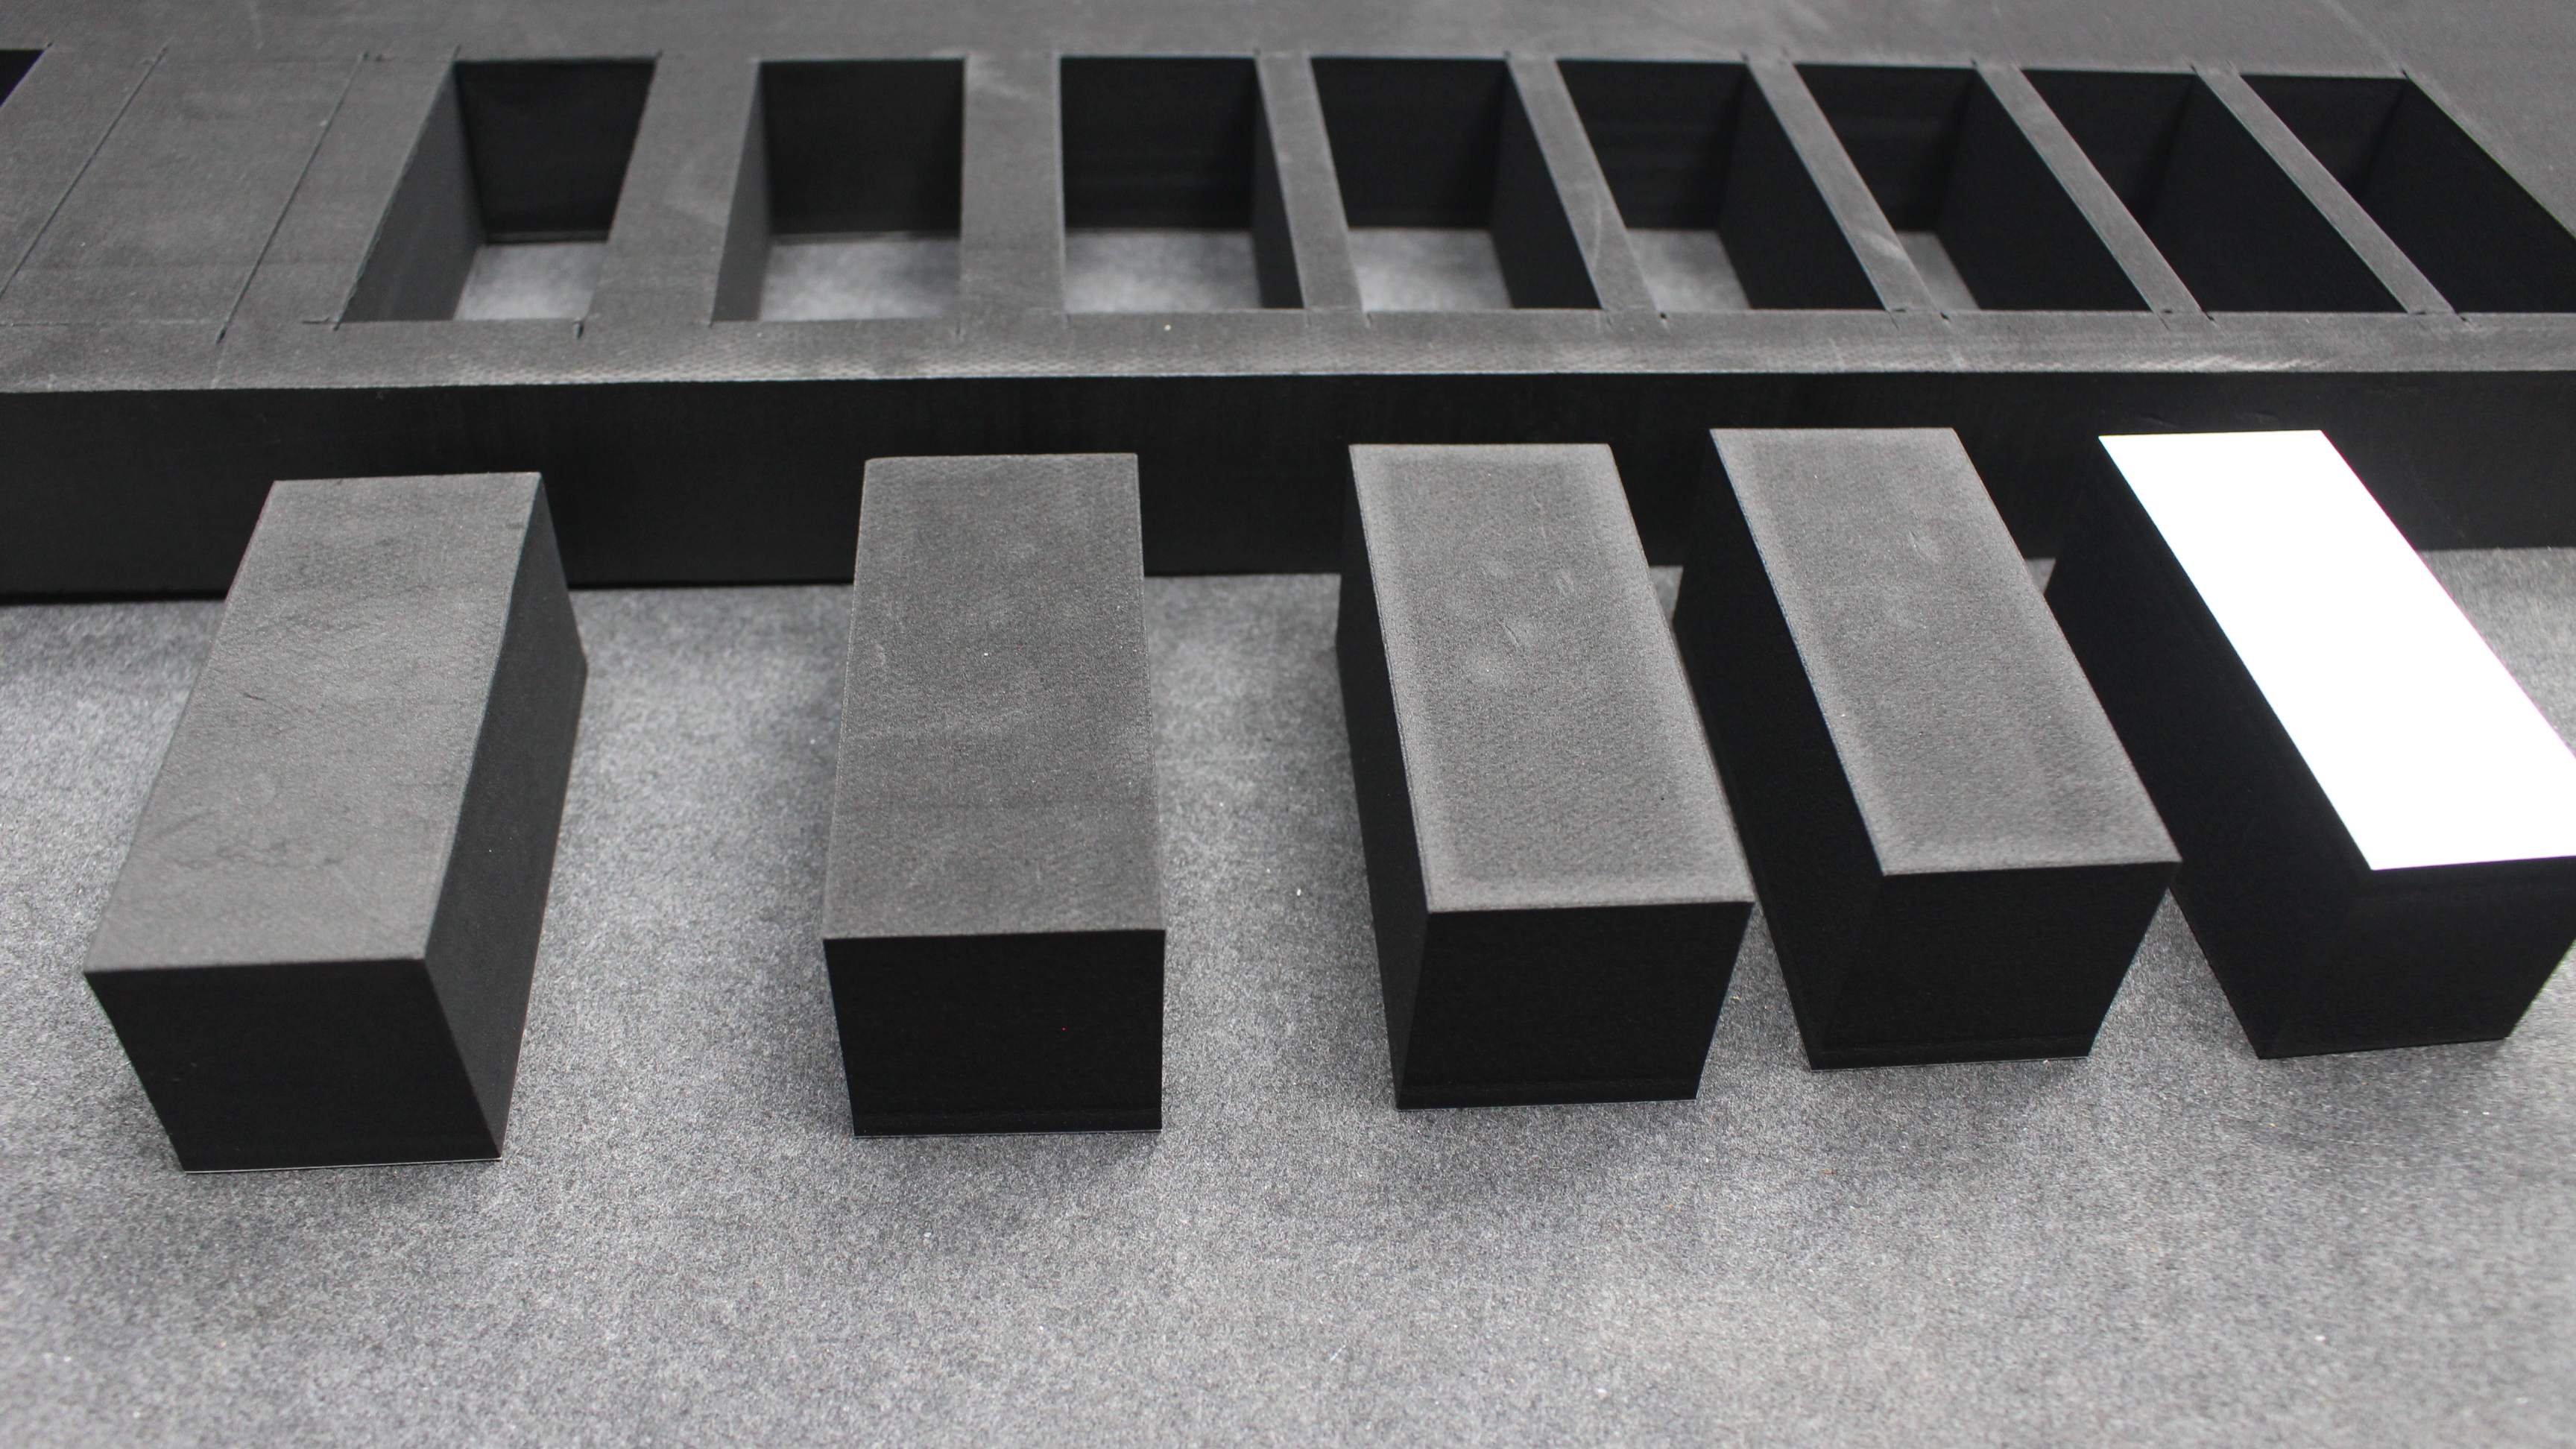
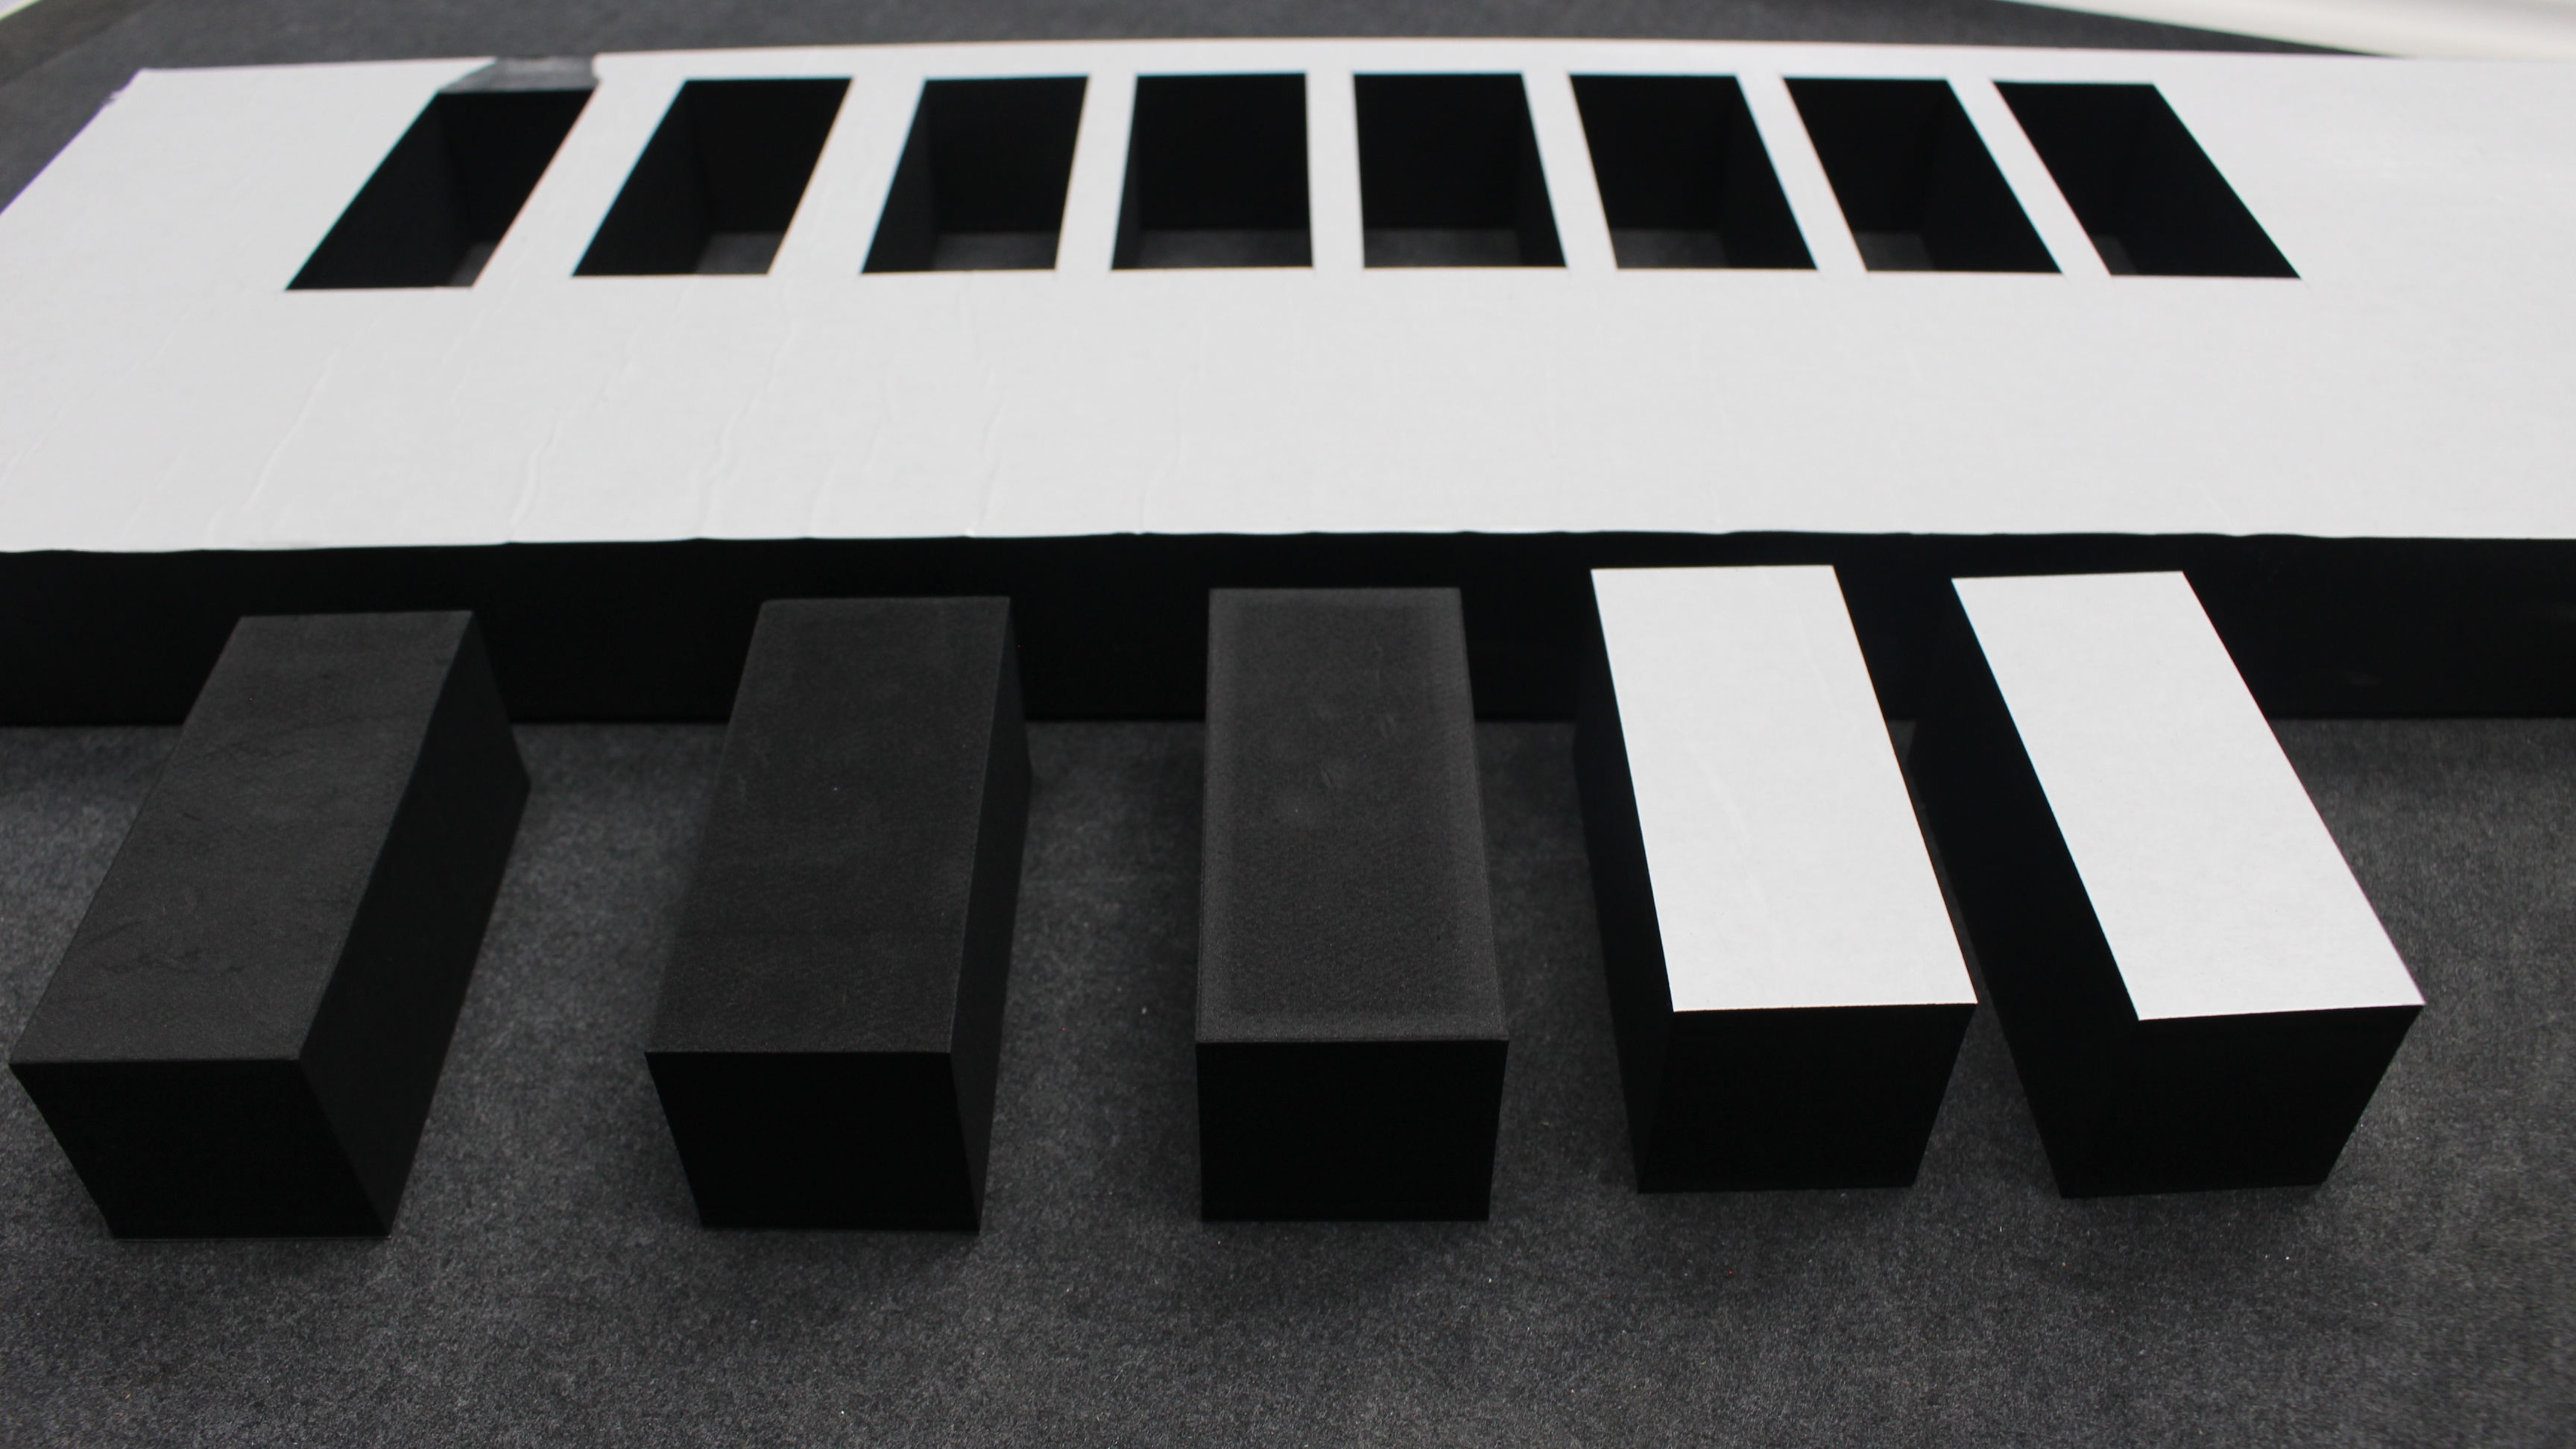
100mm Thick EVA Extreme Thickness Test
For 100mm thick EVA extreme thickness material, the test used ZCRA1410 (with 100mm raised head) equipped with 10mm high-amplitude pneumatic oscillating knife, plus cooling spray system. Actual test findings: blade broke when cutting the second workpiece; waste removal was extremely difficult after thick material cutting. This confirms that EVA thick material processing requires strict evaluation of hardness and cooling conditions.
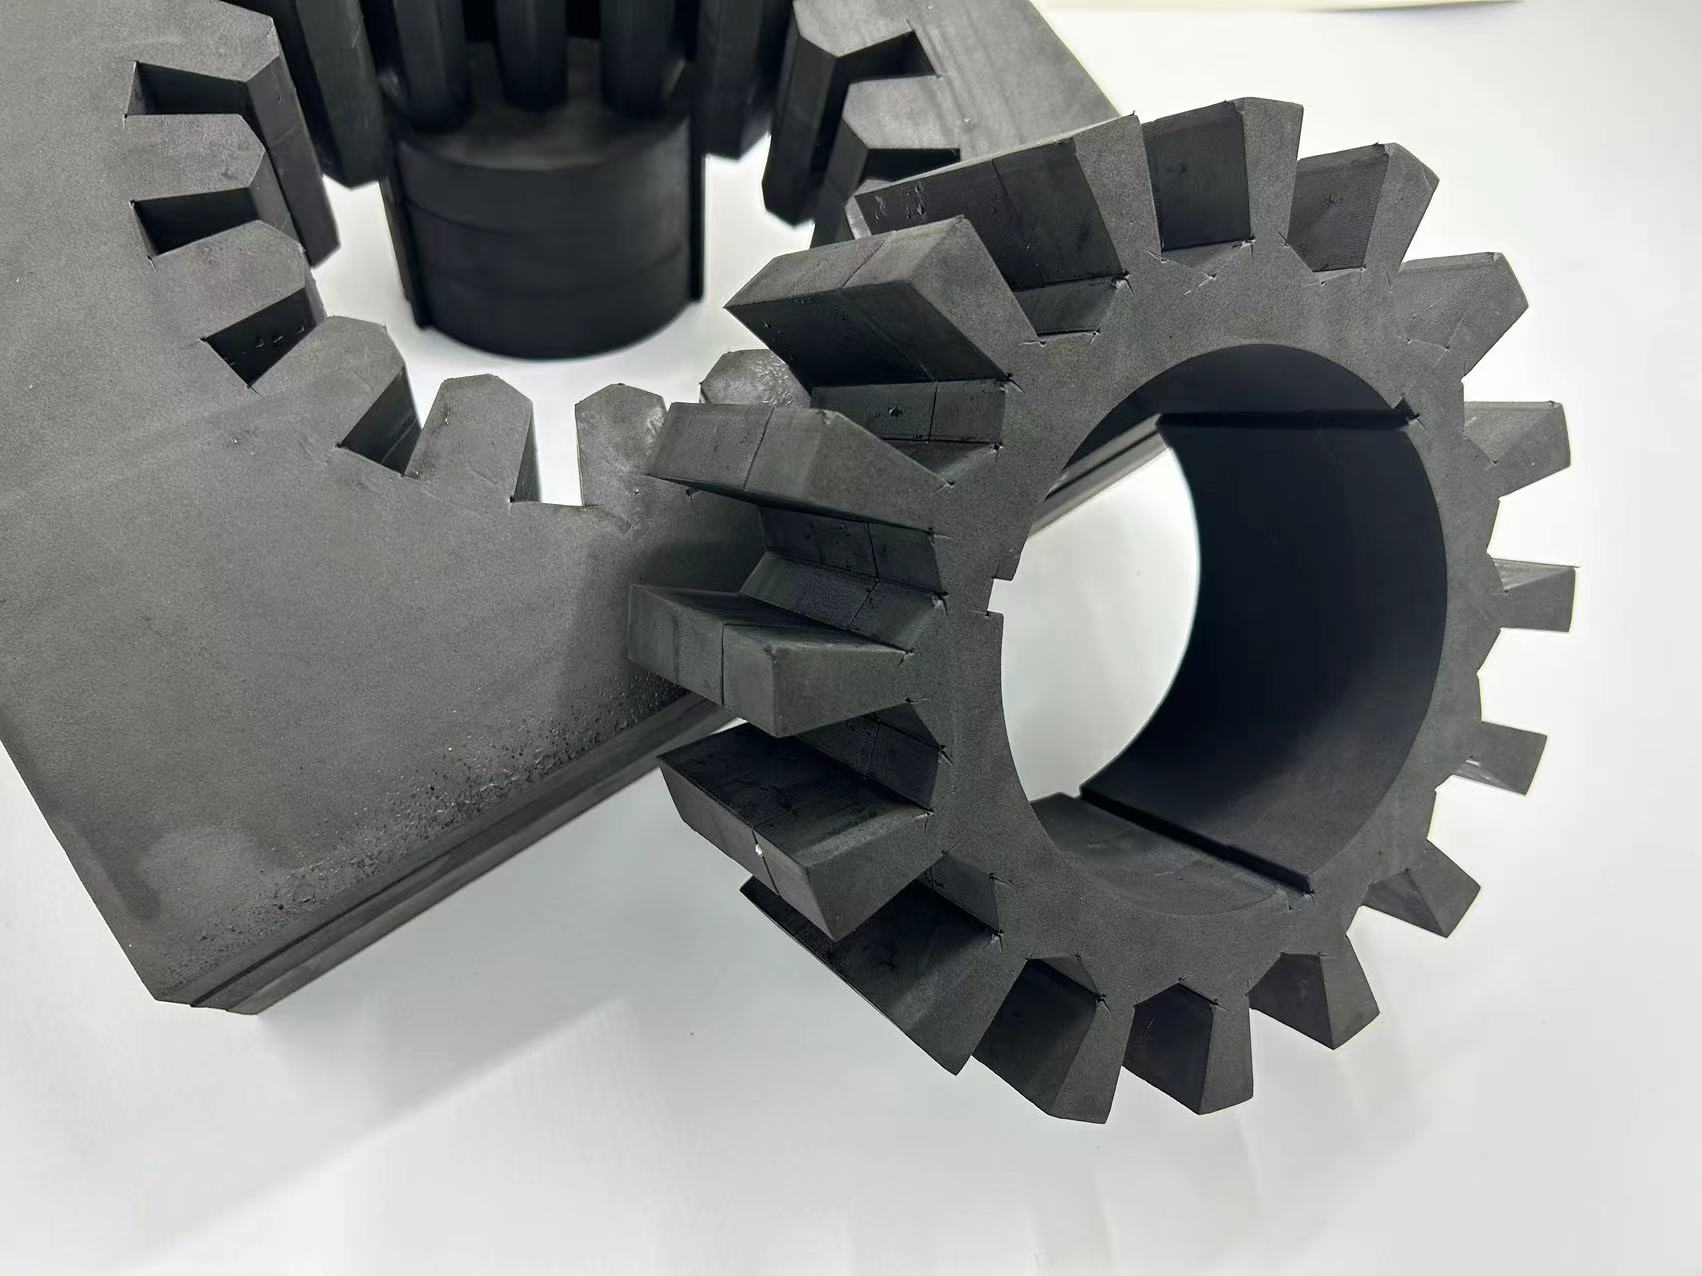
Processing Boundary Explanation
EVA foam cutting requires comprehensive evaluation of hardness, thickness, and cooling conditions:
- Hardness ≥45°: Recommended cutting thickness not exceeding 40mm
- Hardness <45°: Theoretically can cut 0-100mm, but must be paired with raised head, high-amplitude pneumatic knife, and cooling spray system for heat dissipation
- Waste removal process: Thick material cutting recommends adjusting tool seat process (such as V-groove assistance) or evaluating mainstream waste removal solutions from similar machines in the industry
Cutting Process Video
FAQ
Q: What are the recommended parameters for ZCCUTTER equipment cutting EVA thick materials (such as 100mm)?
A: Must be evaluated based on EVA hardness. For hardness above 45°, recommended cutting thickness not exceeding 40mm; for hardness below 45°, theoretically can cut 0-100mm, but must be paired with raised head, high-amplitude pneumatic knife, and cooling spray system for heat dissipation.
Q: How to solve blade breakage and difficult waste removal when cutting 100mm thick EVA?
A: Thick material cutting puts extreme load on the blade, requiring optimization of cooling spray position and flow to extend tool life. For difficult waste removal, it is recommended to adjust tool seat process (such as V-groove assistance) or evaluate mainstream waste removal solutions from similar machines in the industry.
Q: What is the difference between cutting 38°/45°/70° EVA?
A: The lower the hardness, the softer the material, requiring larger tool amplitude and slower downward speed to prevent material deformation; the higher the hardness, the harder the material, requiring higher cutting pressure and tool wear resistance. ZCCUTTER AI1500 process library has built-in parameter presets for different hardness EVA, enabling quick matching of optimal cutting solutions.
Test Disclaimer
This test data comes from real production condition records. Actual cutting results may vary due to material density and hardness differences. ZCCUTTER does not guarantee processing effects beyond the above actual test parameter range.